Sponsored article
Why Does Automatic Deburring Produce Different Results on the Same Sheet Metal?
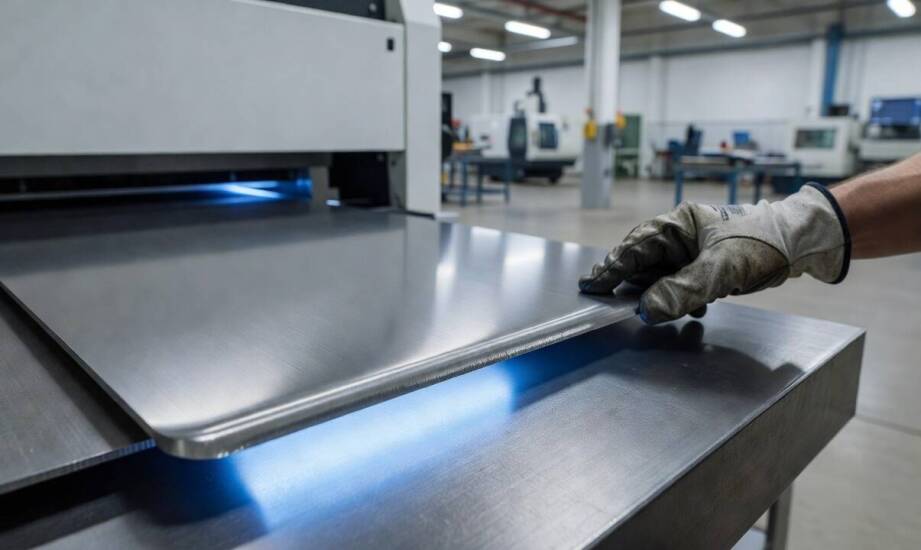
Automatic deburring after cutting does not always deliver identical results, even when the sheet metal comes from the same material batch. Variations in the final surface finish are directly related to the initial condition of the workpiece, particularly the characteristics of the edge left by laser, plasma or waterjet cutting. The parameters of the mechanical finishing process also play a major role and must be carefully matched to the type of burr being removed.
Proper adjustment of abrasive tool pressure, feed speed and machining unit configuration is essential for achieving consistent production quality. Understanding the relationship between the cutting process and the operation of brushes and abrasive tools enables operators to remove sharp edges, eliminate stubborn slag deposits and prepare components for subsequent processes such as bending, welding or powder coating.
How Cutting Technology and Tool Mechanics Influence the Deburring Process
Each thermal or water-based cutting technology affects the structure of the sheet metal edge differently. These differences directly determine the selection of abrasive materials and machining parameters.
Laser cutting typically leaves a thin layer of molten metal, which solidifies into relatively hard and sharp burrs, usually located on the underside of the workpiece. Such deposits often require aggressive machining units with high rigidity.
Plasma cutting creates a larger amount of slag and a wider heat-affected zone. As a result, thicker but often more brittle edge formations appear. If the brushes strike them incorrectly, they may chip away instead of being removed smoothly.
Waterjet-cut material behaves differently. Waterjet technology produces edges free from thermal damage, although thicker sheets may still require micro-irregularities to be smoothed and sharp edges to be rounded.
How Do Deburring Tools Work?
Sheet metal finishing systems rely on three primary machining mechanisms.
Abrasion removes the hardest slag deposits and small metal protrusions created during rapid solidification at the cutting edge.
The process then moves to the main stage: shearing, which mechanically removes larger and more strongly attached burrs.
The final step is edge rounding, performed using flexible rotating discs or transverse brush blocks. This operation removes sharp corners that could injure operators or contribute to coating failures along edges.
The effectiveness of these mechanisms depends heavily on deburring machine settings.
Adjustment of the working pressure determines how deeply the abrasive material engages with the workpiece. Excessive pressure may rapidly wear abrasive media and create unwanted waviness on flat sheet surfaces.
Equally important is the conveyor speed, which directly determines the time the component spends under the machining heads. Slower feed rates extend processing time and facilitate the removal of difficult burrs.
The final machining result is also influenced by the number of active units, their type and their rotational direction relative to the travelling sheet.
How Should You Select the Right Configuration of Deburring Machines?
Modern deburring systems are available in numerous configurations, allowing manufacturers to match machine capabilities to specific production requirements.
The most important selection criteria are working width and the arrangement of machining stations.
Compact 600 mm models, often equipped with two machining units arranged in sequence, are well suited to smaller components and precise one-sided processing. Larger 1000 mm systems, available with three or four machining heads, can perform calibration, scale removal and intensive edge rounding in a single pass. Facilities handling high-volume production often invest in 1500 mm machines capable of processing full-size sheets directly from laser cutting systems.
The modular architecture used in finishing systems manufactured by Madora enables flexible adaptation of the process to sheet thickness and the type of burr being removed.
The Operator's Role in an Automated Deburring Process
Even the most advanced deburring machine requires proper supervision. Operators should regularly inspect components leaving the machining zone.
Overly aggressive spindle settings can leave visible scratches on the surface. In extreme cases, excessive material removal may alter component dimensions. Warning signs include localised discolouration that may indicate overheating and asymmetric marks left by rotating discs.
Insufficient tool pressure can also be problematic. In such situations, residual scale, partially removed burrs or inadequately rounded edges may remain on the component.
A quick visual inspection usually makes it possible to determine whether machining parameters should be adjusted.
Depending on machine design, adjustments may involve changing the position of a machining unit, modifying conveyor speed or altering brush operating parameters. Proper calibration allows the process to be stabilised without lengthy production interruptions.
Consistent Deburring Depends on Multiple Factors
Effective automatic burr removal and edge rounding result from the precise interaction of several technological factors. Machine parameters, cutting technology, abrasive media and machining unit configuration all play an important role.
Clean surfaces and smooth edges are not only a matter of appearance. They also affect workplace safety, the quality of downstream manufacturing operations and the durability of protective coatings applied later in the production process.
As a result, automatic deburring becomes far more than a method of removing burrs. It is a critical stage in preparing sheet metal for further processing. Proper machine setup helps reduce rework, improve operational safety and maintain consistent manufacturing quality.
You might be interested

How the diversity of vegetable offerings affects the competitive advantage of stores

Why choose Pharmaquinone as your vitamin K2 supplier for supplement production?
What Determines the Suitability of Pork Snout Cuts for Gelatin Production and Meat Batter Binding?